
Process, equipment connection and operating requirements
Review how the complete line is arranged, which finished products it supports, how packaging is handled and what factory conditions should be confirmed.
Production process and equipment connection
2200 Automatic Toilet Paper Rewinding, Cutting and Bundling Line
The 2200 Automatic Toilet Paper Rewinding, Cutting and Bundling Line converts jumbo tissue rolls into embossed, perforated, accurately cut and bundled household toilet paper rolls. The documented configuration combines a 2200-type toilet paper rewinding machine, a DT2200 fully automatic high-speed band-saw paper cutter and a pem-500TS toilet roll bundling machine.
The production process covers jumbo roll unwinding, paper feeding, embossing, perforating, rewinding, tail sealing, automatic log cutting, finished-roll conveying, roll arrangement and multi-roll film bundling. Compared with manual cutting and manual bag sealing, this configuration improves downstream continuity and finished-roll consistency.
Jumbo roll loading, initial paper threading and paper-edge alignment still require operator involvement. Operators are also needed for supervision, film replacement, inspection, finished-bundle collection, cleaning and maintenance. The line should therefore not be described as an entirely operator-free system.
Suitable Finished Products
Standard household toilet paper rolls
Embossed toilet paper rolls
Perforated one-ply and multi-ply toilet paper
Toilet paper rolls with cardboard cores
Finished rolls approximately 100 to 170 mm wide for the listed bundler
Finished rolls approximately 90 to 125 mm in diameter for the listed bundler
Automatically arranged multi-roll toilet paper bundles
The finished roll width, diameter, weight, sheet count, number of plies, core diameter, embossing pattern, perforation pitch and number of rolls per bundle must be confirmed before manufacturing begins. The DT2200 cutter has a wider processing range than the pem-500TS bundling machine, so the bundler must be checked separately against the final roll dimensions.
Main Equipment Composition
2200-type toilet paper rewinding machine
Single-layer jumbo roll rear unwind stand
Paper feeding and active guide-roller system
Raw paper break detection system
Embossing unit
Adjustable perforating unit
Synchronous glue-spraying and web-cutting device
PLC and touch-screen control system
DT2200 automatic high-speed band-saw cutter
PLC and servo-controlled log-feeding system
Automatic band-knife grinding mechanism
Finished-roll conveying and arrangement section
pem-500TS toilet roll bundling machine
Electrical control system
Production Process
Jumbo Roll Loading and Unwinding
The jumbo tissue roll is installed on the single-layer rear unwind stand. The documented maximum raw paper width is approximately 2100 mm, the maximum jumbo roll diameter is approximately 1100 mm and the maximum reference jumbo roll weight is approximately 0.5 t. Suitable lifting equipment is required for unloading, storage, installation and replacement. Paper-edge alignment and initial threading are manual. An active guide roller assists stable feeding, while the paper-break detection system monitors the web during operation.
Embossing and Perforating
The paper web passes through embossing and perforating sections before rewinding. The upper perforation blade has an adjustable extension structure. Its position should be adjusted according to paper basis weight, strength, number of plies and the required tear-line quality. The embossing pattern, perforation pitch and ply structure should be confirmed from the approved finished-product sample.
Toilet Paper Rewinding
The processed paper is rewound into long toilet paper logs. The documented operating speed is approximately 80 to 160 m/min. Actual speed depends on raw paper strength, basis weight, number of plies, embossing pressure, perforation, finished diameter and winding firmness. PLC and touch-screen controls are used to set and monitor the principal parameters. The rewinder main motor is approximately 5.5 kW with frequency control.
Web Cutting and Tail Sealing
A synchronous-belt-driven circular cutting and glue-spraying device separates the paper web and seals the tail at the end of each rewinding cycle. Tail-sealing quality depends on glue type, application quantity, paper surface and machine settings. The completed log is then transferred toward the automatic cutter through a transfer section or connecting conveyor confirmed in the final layout.
Automatic High-Speed Log Cutting
The DT2200 automatic band-saw cutter divides long logs into individual rolls. Its documented cutting diameter is approximately 40 to 140 mm and cutting length is approximately 50 to 300 mm. Reference speed is approximately 100 to 150 cuts/min. PLC and servo control position and feed the logs. The reference band-knife size is 3880 × 60 × 0.65 mm, and a stepper-motor mechanism automatically advances the sharpening system.
Finished-Roll Inspection and Conveying
Irregular head and tail sections should be removed before accepted rolls enter the bundling section. Inspection can include width, diameter, weight, cut surface, alignment, embossing, perforation, core position, winding firmness and tail sealing. Accepted rolls are separated, oriented and conveyed according to the selected bundle arrangement. Conveyor speed must be coordinated with both the cutter and bundling machine.
Automatic Multi-Roll Bundling
The pem-500TS bundling machine arranges finished rolls and forms multi-roll film packs. The documented speed is approximately 80 to 120 rolls/min. The listed applicable roll width is approximately 100 to 170 mm, roll diameter is approximately 90 to 125 mm and maximum film width is approximately 450 mm. Package quantity and arrangement are not fixed by the model name and must be confirmed from the product and film specification.
Reference Technical Parameters
| Production Line Name | 2200 Automatic Toilet Paper Rewinding, Cutting and Bundling Line |
|---|---|
| Automation Description | Automatic rewinding, servo cutting and multi-roll bundling with operator-assisted jumbo roll loading, alignment and initial threading |
| Maximum Raw Paper Width | Approximately 2100 mm |
| Maximum Jumbo Roll Diameter | Approximately 1100 mm |
| Maximum Jumbo Roll Weight | Approximately 0.5 t |
| Practical Rewinding Speed | Approximately 80 to 160 m/min |
| Jumbo Roll Feeding | Single-layer rear unwind stand |
| Paper Edge Alignment | Manual |
| Initial Paper Threading | Manual |
| Paper Break Detection | Included |
| Perforation Blade | Adjustable upper-blade extension |
| Rewinder Main Motor | Approximately 5.5 kW with frequency control |
| Compressed-Air Pressure | Approximately 0.45 to 0.60 MPa |
| Reference Air Consumption | Approximately 40 m³ per shift for the listed rewinder |
| Automatic Cutter Model | DT2200 |
| Cutting Diameter | Approximately 40 to 140 mm |
| Cutting Length | Approximately 50 to 300 mm |
| Cutting Speed | Approximately 100 to 150 cuts/min |
| Band-Knife Size | Approximately 3880 × 60 × 0.65 mm |
| Knife Grinding Control | Stepper-motor-controlled automatic feed |
| Log Feeding Control | PLC and servo motor |
| Cutter Main Motor | Approximately 4.5 kW |
| Bundling Machine Model | pem-500TS |
| Bundling Speed | Approximately 80 to 120 rolls/min |
| Applicable Roll Width | Approximately 100 to 170 mm |
| Applicable Roll Diameter | Approximately 90 to 125 mm |
| Maximum Film Width | Approximately 450 mm |
| Recommended Operators | Approximately 2 to 4 people per shift |
| Power Supply | Three-phase industrial power, customized for destination voltage and frequency |
The listed parameters are based on the supplied equipment document. Final values must follow the signed technical agreement, approved drawings, electrical list, finished-roll specification and connecting-conveyor design.
Equipment Dimensions and Weight
| 2200-Type Toilet Paper Rewinding Machine | Approximately 5500 × 3500 × 1750 mm; approximately 2200 kg |
|---|---|
| DT2200 Automatic Band-Saw Cutter | Approximately 4200 × 900 × 2200 mm; approximately 1200 kg |
| pem-500TS Toilet Roll Bundling Machine | Approximately 6000 × 2800 × 1600 mm; machine weight to be confirmed |
The source material contains inconsistent dimension wording for the rewinder. Final dimensions must follow the approved equipment drawing. Additional space is required for jumbo roll replacement, log transfer, conveyors, film replacement, maintenance and finished-product collection.
Automation and Operator Involvement
The line automates the principal rewinding, cutting and bundling stages while retaining necessary operator-assisted work.
Automatic functions: normal web feeding, paper-break detection, embossing, perforating, rewinding, glue spraying, web cutting, tail sealing, servo log feeding, band-saw cutting, sharpening feed, roll conveying, arrangement and bundling
Operator-assisted functions: jumbo roll handling, initial threading, edge alignment, parameter confirmation, quality inspection, film replacement, finished-product collection, cleaning and maintenance
Recommended Operator Arrangement
A normal shift can use approximately two to four operators.
One operator for jumbo roll loading, threading and rewinder supervision
One operator for cutter monitoring and cut-quality inspection
One operator for film replacement and bundle inspection
One additional operator for raw-material handling and finished-product collection when required
Practical Output
The stage speeds use different measurement units and cannot be treated as one guaranteed line-output figure.
Finished roll width, diameter, weight and sheet count
Paper plies, basis weight and strength
Embossing pressure and perforation pitch
Log length and rolls cut from each log
Knife condition and cutting accuracy
Conveyor arrangement and bundle format
Film specification, jumbo roll replacement and maintenance time
Workshop and Utility Requirements
A practical installation should arrange the equipment in sequence and provide sufficient storage, access and maintenance space.
Recommended line area: approximately 22 to 28 m long and 6 to 8 m wide
Recommended total workshop area: approximately 250 to 400 m²
Clear height: at least 4 m
Level industrial floor and suitable jumbo roll lifting equipment
Three-phase industrial power
Compressed air at approximately 0.45 to 0.60 MPa
Raw paper, film and finished-product storage
Safe access and maintenance clearance around all equipment
Standard Delivery Scope
The principal documented equipment includes the following items. Final supply boundaries must be reconfirmed in the quotation.
One 2200-type rewinding machine and rear unwind stand
Embossing, perforating, glue-spraying and web-cutting sections
PLC and touch-screen control system
One DT2200 automatic band-saw cutter with servo feeding and automatic sharpening feed
One pem-500TS bundling machine
Electrical control components for the listed equipment
Information Required for Final Configuration
The following data are required before the line is finalized.
Finished roll width, diameter, weight and sheet count
Paper plies, basis weight and jumbo roll dimensions
Perforation pitch, core diameter and embossing pattern
Number and arrangement of rolls per bundle
Film material, thickness, width and printed-film requirements
Required hourly or shift output
Available operators and workshop dimensions
Destination voltage, frequency and compressed-air conditions
Power Configuration
The known motor power is approximately 10 kW, consisting of the 5.5 kW rewinder motor and the 4.5 kW cutter motor. This is not the total installed power of the complete line. The bundling machine, conveyors, auxiliary drives, air compressor and optional equipment must be added after the final electrical list is approved.
Configuration Note
The model designation 2200 does not mean that the documented maximum raw paper width is 2200 mm. The supplied parameter sheet lists a maximum width of approximately 2100 mm. The source also contains inconsistent design-speed and dimension wording, so final manufacturing values must follow the signed technical agreement and approved drawings.
A guaranteed finished output should only be stated after the finished-roll specification, number of rolls per bundle, conveyor arrangement and packaging-film specification are confirmed and the three principal stages are checked as one balanced production system.
Primary and secondary packing options
Equipment arrangement and workshop flow
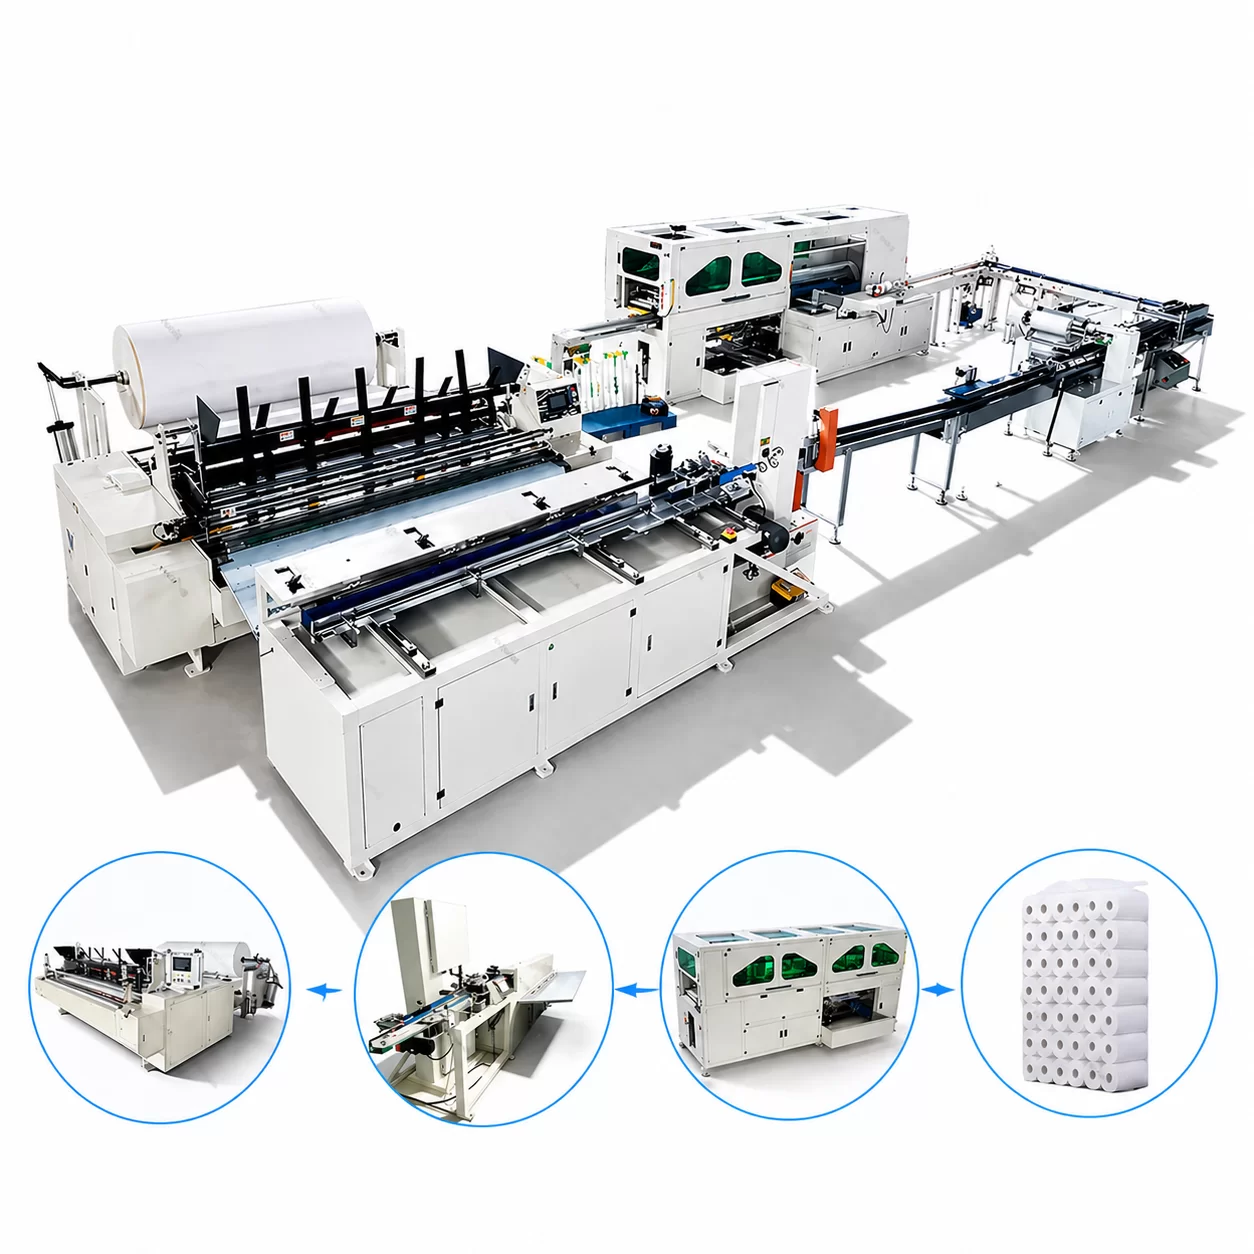
Practical output, operator quantity, installed power and workshop space depend on the final equipment combination, finished-product dimensions, packing format and operating conditions. Confirm these values in the final technical proposal.