
Process, equipment connection and operating requirements
Review how the complete line is arranged, which finished products it supports, how packaging is handled and what factory conditions should be confirmed.
Production process and equipment connection
The 2200 mm Fully Automatic Kitchen Towel Production Line converts jumbo tissue rolls into embossed, perforated, cut and packed kitchen towel rolls. The connected configuration reduces repeated manual handling between rewinding, cutting, conveying and packaging.
The line is suitable for two-ply and three-ply kitchen towel rolls, deep-embossed kitchen paper, laminated paper towels, individually wrapped rolls and multi-roll retail packs. The final equipment configuration is selected according to the raw paper, finished roll size, sheet count, embossing pattern, output and packaging method.
Production Process
Jumbo tissue rolls are installed on two or three unwind stands. The paper webs pass through the tension-control and web-guiding systems before entering the embossing section.
The embossing units form the required surface pattern and improve the thickness and appearance of the kitchen towel. A glue lamination system can be added to bond two or three embossed plies and reduce ply separation.
After embossing and lamination, the paper is perforated and rewound into long kitchen towel logs. The rewinder controls the sheet length, sheet count, roll diameter, winding firmness, core feeding and tail sealing.
Completed logs are discharged automatically and transferred to an accumulation system. The automatic log saw then cuts each log into finished kitchen towel rolls. Cut rolls are separated, counted and conveyed to the selected packaging machine.
Main Equipment
Two or three jumbo roll unwind stands
Automatic web-guiding and tension-control system
Double embossing units
Glue lamination system
2200 mm automatic kitchen towel rewinder
Automatic core feeding and tail-sealing system
Log accumulation and transfer conveyors
Servo-controlled automatic log saw
Finished-roll separation and counting system
Individual roll wrapper or multi-roll packing machine
Finished-pack discharge conveyor
PLC control cabinets and safety protection devices
Reference Parameters
Effective working width: 2200 mm
Practical rewinding speed: 130 to 180 m/min
Finished-roll output: approximately 80 to 150 rolls/min
Production capacity: approximately 3.5 to 6 tons per 8-hour shift
Finished roll width: 220 to 280 mm
Finished roll diameter: 100 to 160 mm
Paper plies: 2 to 3 plies
Raw paper basis weight: 16 to 30 g/m² per ply
Perforation length: 180 to 300 mm
Maximum jumbo roll diameter: 1500 to 2000 mm
Installed power: approximately 70 to 105 kW
Operators: 4 to 6 people per shift
Compressed-air pressure: 0.6 to 0.8 MPa
Packaging Formats
The line can be configured for individual roll wrapping, two-roll packs, four-roll packs, six-roll packs, customized multi-roll bags, bundle packing or carton handling.
The packaging equipment must be selected according to the finished roll width, roll diameter, number of rolls per pack, film specification and required packing speed. Different pack arrangements require different grouping and feeding systems.
Automation and Operators
The line can automatically complete embossing, lamination, perforating, rewinding, core feeding, tail sealing, log discharge, log cutting, roll conveying, product counting and primary packaging.
The production line still requires 4 to 6 operators for jumbo roll replacement, core and film replenishment, glue preparation, product inspection, specification changeover, cleaning, fault handling and routine maintenance.
Workshop Requirements
The recommended production line footprint is approximately 32 to 40 m long and 10 to 12 m wide. A total workshop area of 600 to 850 m² and a clear height of at least 4.5 m are recommended.
The workshop layout should reserve space for jumbo roll storage, packaging materials, finished-product collection, operator passages, electrical cabinets and equipment maintenance. The final layout must also consider doors, columns, material flow and utility connection points.
Information Required for Configuration
Before confirming the line, please provide the finished roll width and diameter, roll weight, number of plies, paper basis weight, sheet length, sheets per roll, core diameter, embossing pattern, jumbo roll dimensions, required output, packaging format, workshop drawing and destination voltage.
The final production capacity, installed power, operator quantity and line dimensions will be confirmed according to the selected raw material, finished kitchen towel specification and packaging configuration.
Primary and secondary packing options
Equipment arrangement and workshop flow
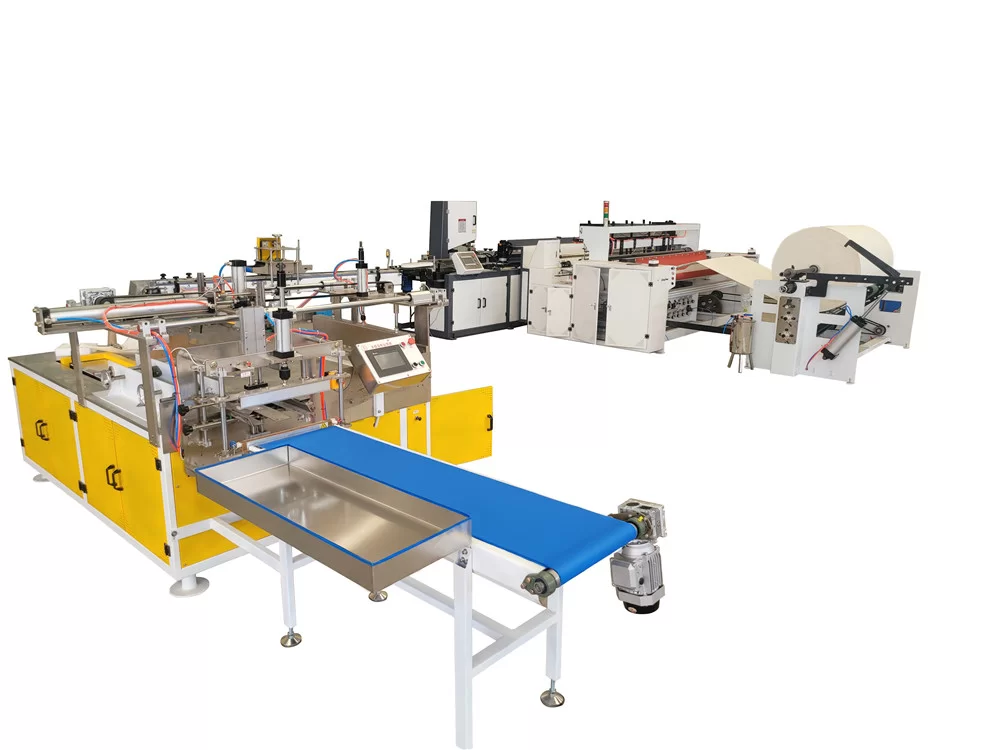
Practical output, operator quantity, installed power and workshop space depend on the final equipment combination, finished-product dimensions, packing format and operating conditions. Confirm these values in the final technical proposal.